Gas & Steam Turbine Nozzle Guide Vane (NGV) & Diaphragm Castings: Cobalt-Base Superalloys, Ceramic Coring, and 5-Axis Airfoil Machining
2026-09-27
Meta Description: A complete technical guide to industrial gas and steam turbine stationary nozzle guide vane (NGV), segment, and diaphragm castings. Explore Cobalt-base superalloys (FSX-414, X-40), Nickel-base alloys (Inconel 718, IN-939, IN-738LC), ceramic core serpentine cooling channels, vacuum investment casting, 5-axis CNC airfoil milling, and Level 4 fluorescent penetrant inspection.
In heavy-duty industrial gas turbines (IGT), aero-derivative turbines, turbo-expanders, and high-pressure steam turbines, stationary Nozzle Guide Vanes (NGVs), Stator Vane Segments, and Diaphragm Partitions operate at the thermodynamic epicenter of the power cycle. Positioned directly downstream of the combustor exit:
- Stage 1 & Stage 2 Gas Turbine Nozzle Guide Vanes: Direct blazing combustion gas streams at temperatures ranging from 850\text{ °C} to } 1,150\text{ °C} (1,560\text{ °F} to } 2,100\text{ °F}) and velocities exceeding onto rotating turbine blades, enduring intense aerodynamic gas bending moments, violent thermal shock during rapid startup, high-temperature oxidation, and Type I/II hot corrosion attack from sulfur and alkali contaminants.
- Steam Turbine HP/IP Diaphragm Vane Rings: Channel supercritical steam at pressures up to , enduring steam droplet erosion-washout, high-temperature creep, and diaphragm dishing deflections.
Under these extreme conditions, vane trailing-edge cracking, thermal fatigue warping, or throat area constriction will degrade turbine heat rates, spike fuel consumption by millions of dollars per year, or cause catastrophic downstream rotating blade impact destruction.
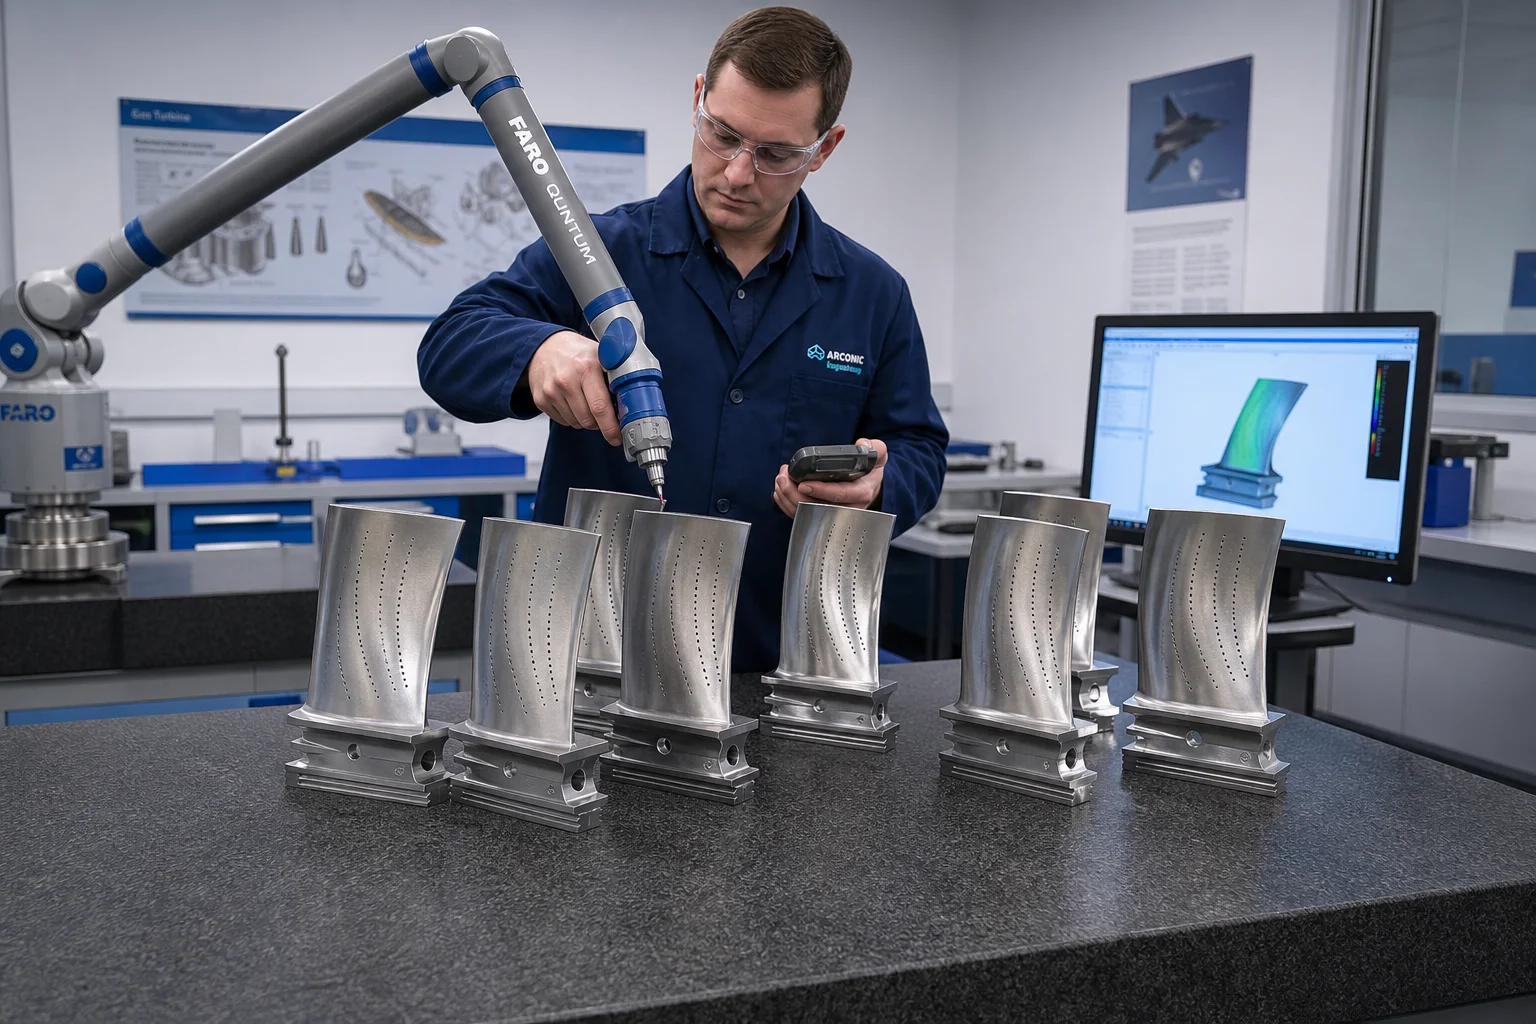
Achieving extreme reliability demands specialized superalloy investment casting: casting Cobalt-Base Superalloys (ASTM A567 Grade 1 / FSX-414 / X-40) for superior hot corrosion and thermal fatigue resistance, Nickel-Base Superalloys (Inconel 718 / IN-939 / IN-738LC) for high creep rupture strength, integrating Multi-Piece Leachable Ceramic Cores for internal serpentine air cooling passages, executing high-speed 5-axis CNC airfoil contouring ( throat profile accuracy), and verifying surface integrity through Fluorescent Liquid Penetrant Inspection (ASTM E1417 Level 4).
This technical guide provides an exhaustive engineering breakdown of superalloy metallurgy, ceramic core investment casting, vacuum melting protocols, 5-axis CNC airfoil machining, and quality assurance workflows.
1. Operating Aerothermal Stress Fields & Failure Modes
 ┌──────────────────────────────────────────────┐
                     │ Blazing Hot Gas Stream (850 °C - 1150 °C)    │
                     └──────────────────────┬───────────────────────┘
                                            │
        ┌───────────────────────────────────┼───────────────────────────────────┐
        ▼                                   ▼                                   ▼
┌───────────────────────────────┐ ┌───────────────────────────────┐ ┌───────────────────────────────┐
│ Trailing-Edge Thermal Fatigue │ │ Type I & II Hot Corrosion     │ │ Gas Bending Creep Deflection  │
│ (Rapid thermal gradients      │ │ (Alkali sulfate $Na_2SO_4$    │ │ (Aerodynamic pressure pushing │
│  causing trailing edge cracks)│ │  fluxing protective oxides)   │ │  vane trailing edge over time)│
└───────────────────────────────┘ └───────────────────────────────┘ └───────────────────────────────┘| Turbine Component | Working Temperature & Environment | Critical Failure Mode to Prevent | Superalloy Solution |
|---|---|---|---|
| Stage 1 Gas Turbine Nozzle Guide Vane (NGV) | / Combustor gas exit | Thermal fatigue cracking, leading-edge burn-through | Cobalt-Base Superalloy (FSX-414 / ECY-768) with internal cooling |
| Stage 2 & 3 Turbine Vane Segments | / High aerodynamic load | High-temperature creep deflection, hot corrosion | Nickel-Base Superalloy (IN-939 / IN-738LC / Inconel 718) |
| HP/IP Steam Turbine Diaphragm Partitions | / Supercritical steam () | Solid particle erosion, diaphragm dishing sag | 12Cr Martensitic Stainless Steel (AISI 422 / 1.4923 / X22CrMoV12-1) |
| Combustor Transition Ducts & Seal Rings | / Pulsating combustion acoustics | Low-cycle acoustic fatigue, seal fretting | Cast Hastelloy X / Inconel 625 |
2. Superalloy Metallurgy: Cobalt-Base vs. Nickel-Base Systems
A. Cobalt-Base Superalloys: FSX-414 & X-40 (ASTM A567 Grade 1)
For stationary nozzle guide vanes, Cobalt-base alloys outperform Nickel-base alloys in three critical areas:
- Superior Hot Corrosion Resistance: High chromium () forms an impenetrable, self-healing chromia protective barrier that resists aggressive alkali sulfate () attack from low-grade fuels.
- Thermal Shock & Thermal Fatigue Superiority: Lower thermal expansion coefficients and higher melting points () prevent trailing-edge thermal fatigue cracking during rapid turbine startups.
- Solid Solution & Carbide Strengthening: Solid-solution strengthening from Tungsten () combined with stable and carbides pinned along grain boundaries.
| Chemical Element | FSX-414 Target (wt%) | X-40 Target (wt%) | Critical Metallurgical Role |
|---|---|---|---|
| Carbon (C) | Forms boundary carbides; controls creep strength | ||
| Chromium (Cr) | Critical: Imparts maximum hot corrosion and oxidation resistance | ||
| Nickel (Ni) | Stabilizes face-centered cubic (FCC) cobalt austenite matrix | ||
| Tungsten (W) | Heavy refractory atom solid-solution strengthening | ||
| Cobalt (Co) | Balance () | Balance () | High-temperature base matrix with high melting point |
B. Nickel-Base Superalloys: Inconel 718 & IN-939
Where high mechanical tensile and creep rupture strength is required at , and Precipitation-Hardened Nickel-Base Alloys are deployed:
- Inconel 718 (ASTM A567 Gr 12 / N07718): Hardened by coherent body-centered tetragonal (BCT) () precipitates; delivers extreme yield strength ( at ).
- IN-939 (Cast 22.5Cr-19Co-2Ti-1.4Al-1.4Ta-1.0Nb): Optimized for heavy industrial gas turbine vanes, combining high chromium for hot corrosion resistance with high-volume precipitates for long-term creep resistance up to .
3. Precision Vacuum Investment Casting with Serpentine Ceramic Cores
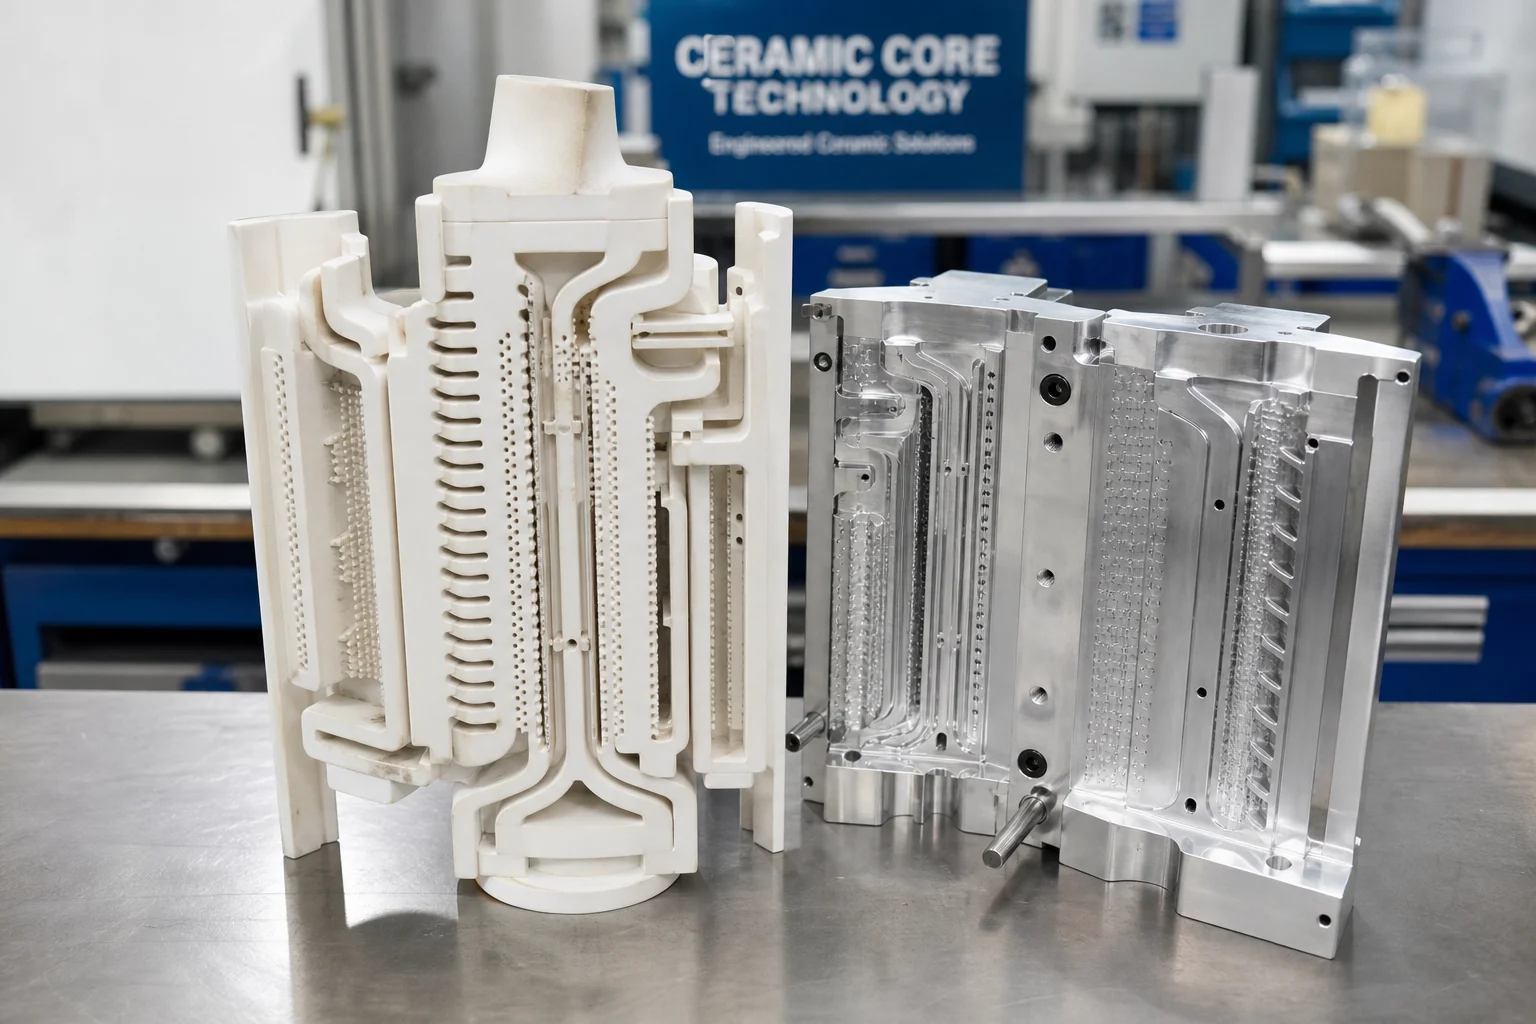
Advanced Stage 1 turbine guide vanes feature hollow airfoils containing intricate internal Serpentine Cooling Passages, Turbulator Ribs, and Trailing-Edge Discharge Pin Fins:
┌─────────────────────────────────────────────────────────────┐
│ 1. Injection of High-Precision Fused Silica / Zirconia Cores│
│    • Intricate serpentine cooling channels (wall gap 1.2 mm)│
├─────────────────────────────────────────────────────────────┤
│ 2. Precision Wax Pattern Assembly & Platinum Pin Positioning│
│    • Ceramic cores locked inside wax vane patterns          │
├─────────────────────────────────────────────────────────────┤
│ 3. Automated Multi-Layer Zircon/Alumina Ceramic Shelling    │
│    • Fine refractory slurry delivers Ra 1.6 µm airfoil finish│
├─────────────────────────────────────────────────────────────┤
│ 4. Vacuum Induction Melting & Pouring (VIM)                 │
│    • High-vacuum chamber ($10^{-3}\text{ mbar}$); zero trace dross │
│    • Directional progressive solidification across airfoil  │
├─────────────────────────────────────────────────────────────┤
│ 5. Autoclave Caustic Core Leaching                          │
│    • High-pressure fused KOH leaching dissolves ceramic     │
│      cores, leaving clean, unobstructed internal air ducts  │
└─────────────────────────────────────────────────────────────┘
4. Multi-Axis 5-Axis CNC Airfoil Machining & EDM Air Hole Drilling
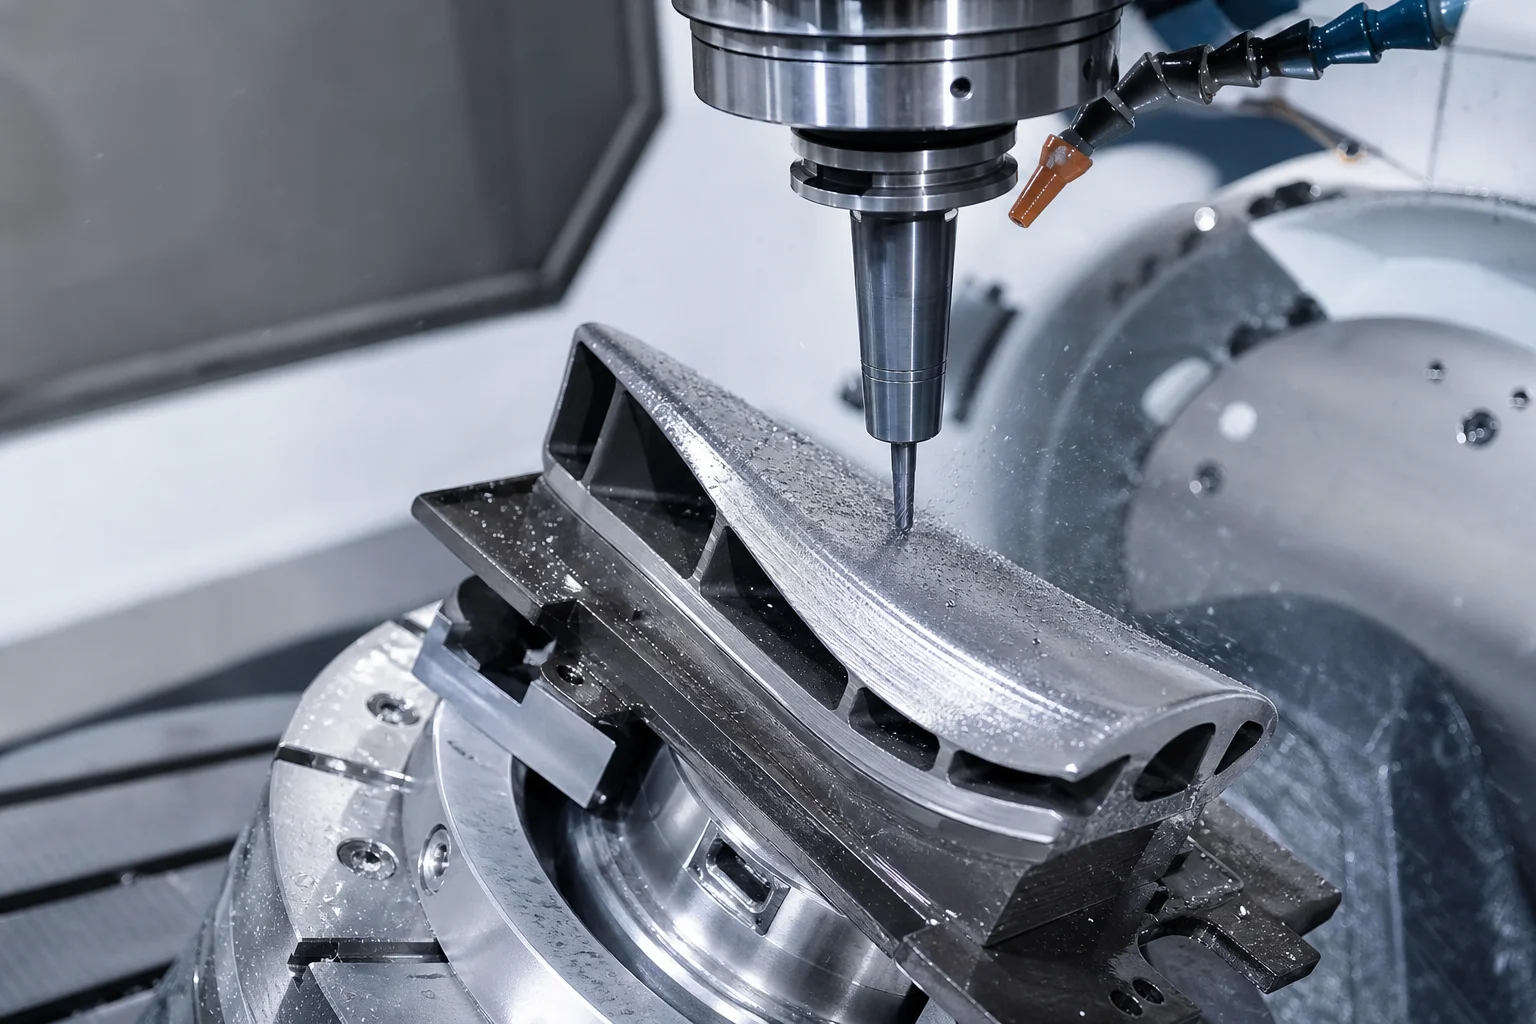
Turbine efficiency and flow aerodynamics depend strictly on vane throat area () and trailing-edge profile accuracy:
 ┌───────────────────────────────────────────────────────┐
        │ 1. Vacuum Solution & Precipitation Heat Treatment     │
        │ • 1,120 °C – 1,180 °C Vacuum Solution + Age Hardening │
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 2. 5-Axis CNC High-Speed Airfoil Milling              │
        │ • Precision milling of root/tip mounting platforms    │
        │ • Complex 3D curved pressure & suction airfoil faces  │
        │ • Airfoil contour tolerance within $\pm 0.025\text{ mm}$   │
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 3. Multi-Axis Fast-Hole EDM & Laser Drilling          │
        │ • Drilling hundreds of micro cooling film holes       │
        │   (Diameter $0.40 – 0.80\text{ mm}$) at angled vectors  │
        │ • Trailing edge cooling slot EDM discharge            │
        └───────────────────────────────────────────────────────┘
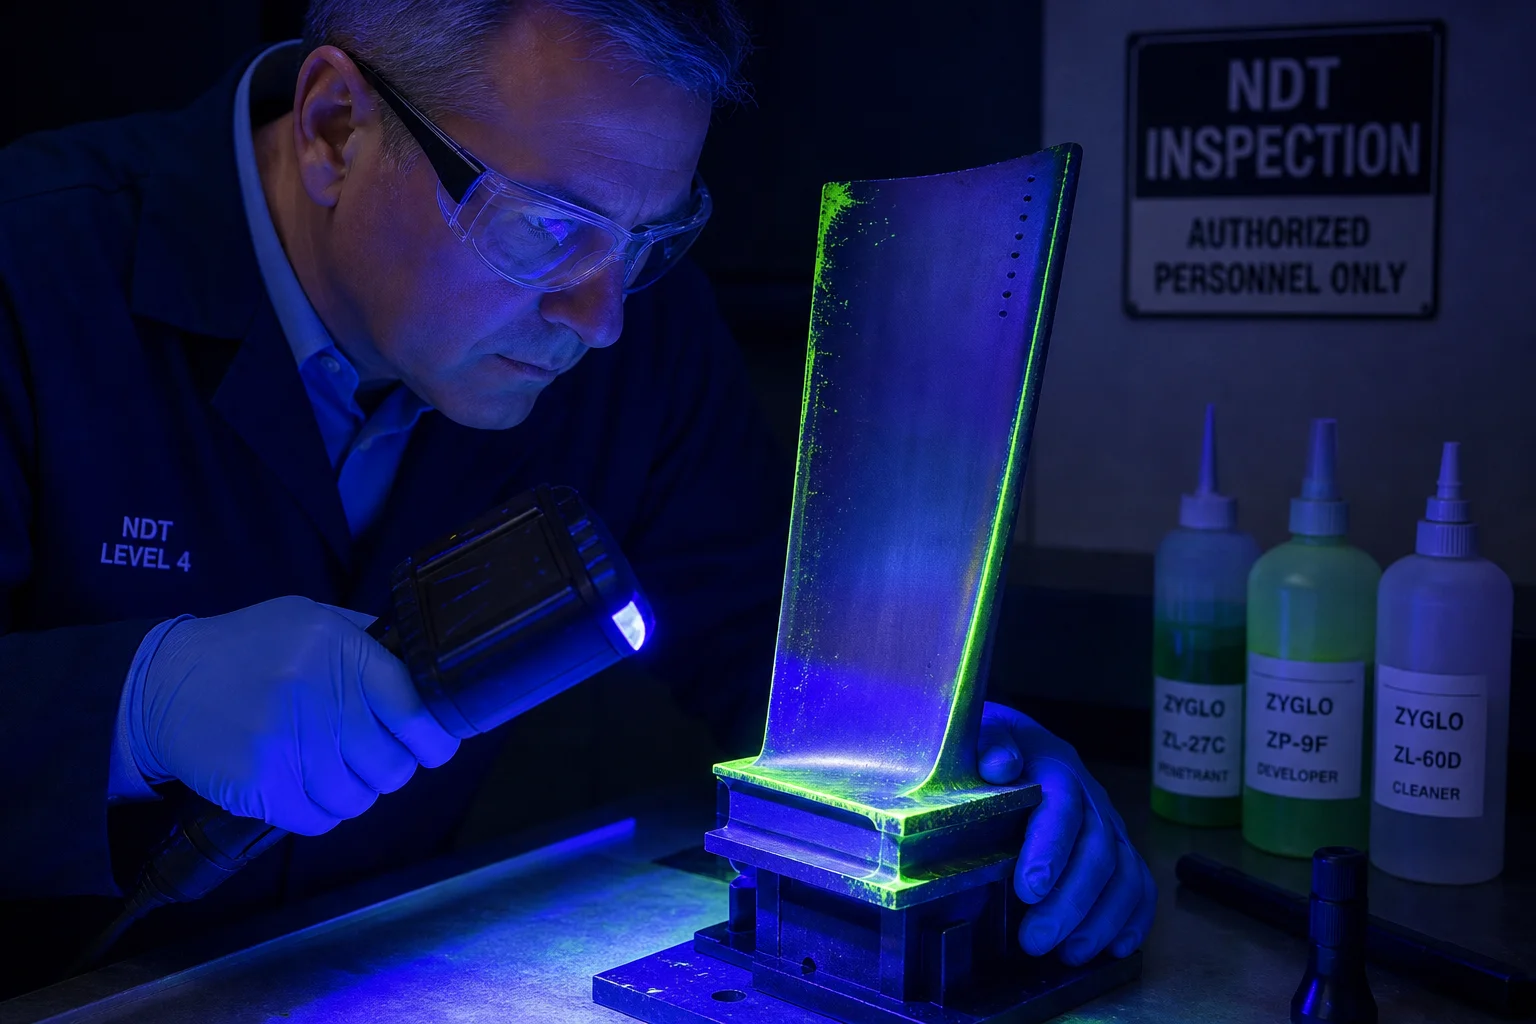
5. Non-Destructive Testing (NDT) & Aerospace-Grade Quality Standards
| Quality Inspection Category | Standard / Test Specification | Acceptance Criteria |
|---|---|---|
| Fluorescent Penetrant (PT) | ASTM E1417 / ISO 3452 Level 4 (Ultra-High) | 100% inspection of leading and trailing edges; Zero Linear Crack Indications |
| Radiographic Testing (RT) | ASTM E192 / ASTM E1030 (Micro-Focus X-Ray) | 100% volumetric inspection of hollow airfoil walls and platforms; Level 1 zero core shift |
| Airflow & Core Passage Test | Mass Flow Airflow Calibration Rig | Internal cooling channel mass flow rate calibrated within of design specification |
| Wall Thickness Ultrasonic Scan | High-Frequency Ultrasonic Gauge () | Airfoil suction and pressure wall thickness within |
| 3D Optical Airfoil Scan | 3D Optical Scanner (ATOS / GOM) | Full 3D color-map inspection against master CAD model; throat area () |
6. Turbine Vane Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
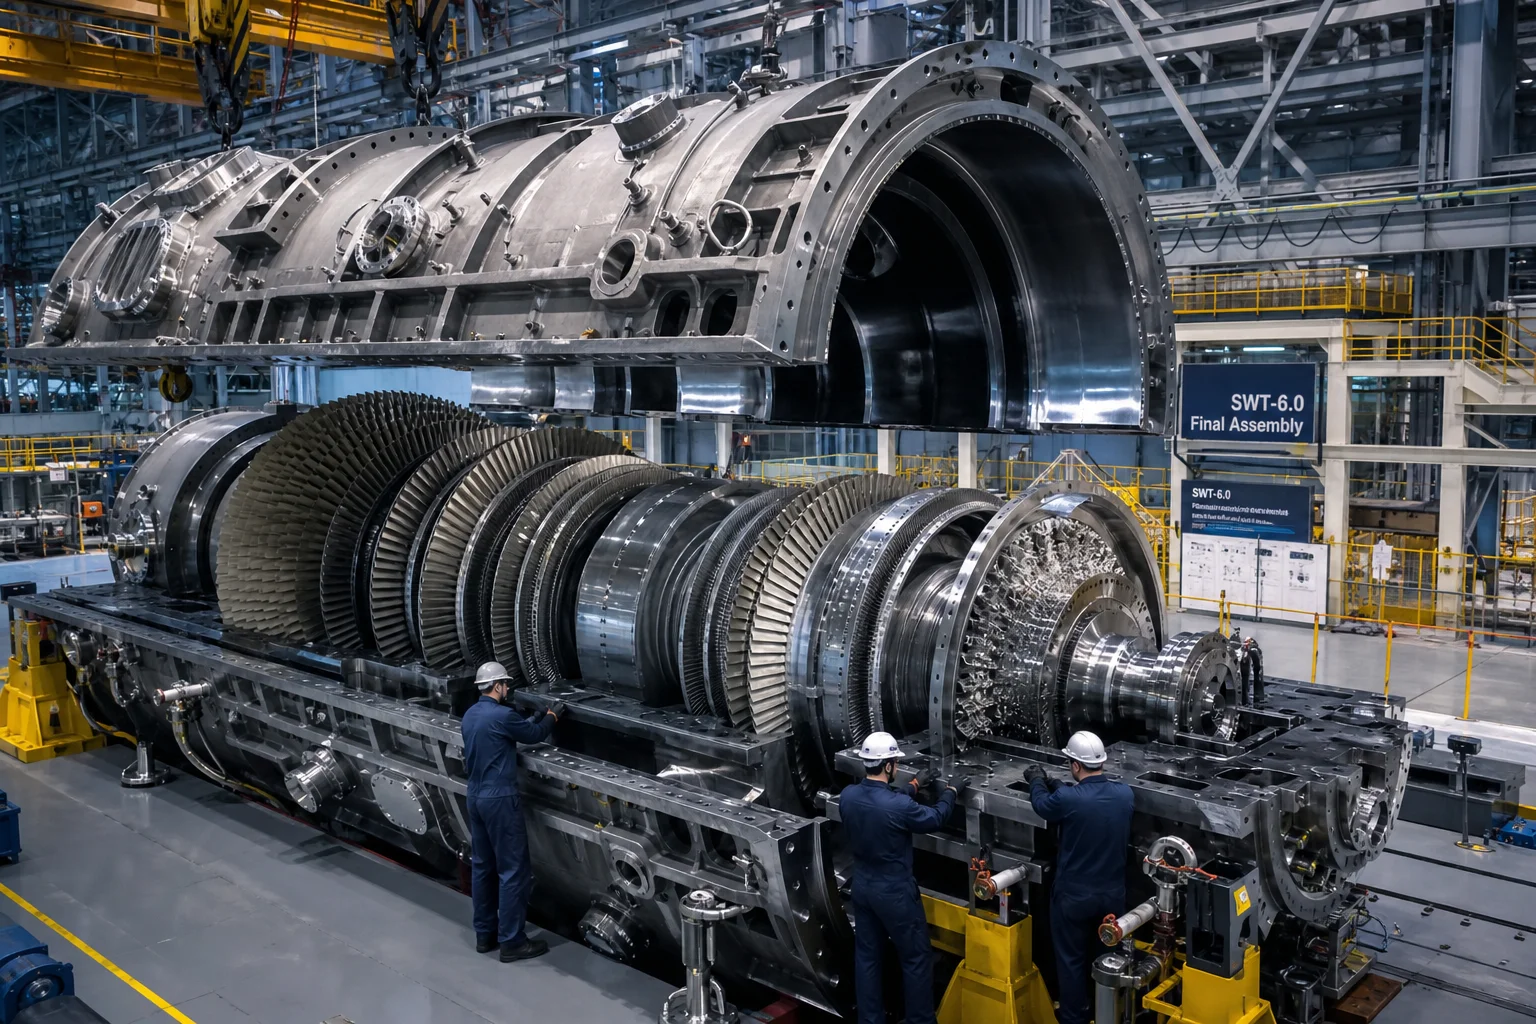
Manufacturing high-temperature gas and steam turbine guide vanes requires specialized vacuum induction melting furnaces, precision ceramic core investment casting shops, 5-axis CNC machining centers, and aerospace-grade NDT inspection laboratories.
Dandong City Pengxin Machinery Co., Ltd. delivers fully certified, precision-machined turbine nozzle guide vanes, vane segments, and diaphragm assemblies:
- Superalloy Metallurgical Mastery: Certified vacuum investment casting of Cobalt-base superalloys (FSX-414, X-40, ECY-768), Nickel-base superalloys (Inconel 718, IN-939, IN-738LC), and 12Cr steels (1.4923 / AISI 422).
- Complex Ceramic Core Technology: Precision ceramic core tooling producing complex serpentine cooling channels with thin wall sections.
- Advanced 5-Axis CNC Machining & EDM: High-precision 5-axis machining centers delivering airfoil contour accuracy within , accompanied by fast-hole EDM film cooling drilling.
- Aerospace-Grade NDT & Flow Testing: Certified Level II/III NDT inspectors conducting 100% Level 4 fluorescent PT, digital micro-focus X-ray, and calibrated mass airflow testing.
- Complete Certification: ISO 9001 certified, providing full EN 10204 3.1 & 3.2 material test certificates, 3D optical scanning reports, and airflow test charts.
Conclusion
Gas and steam turbine nozzle guide vane (NGV) and diaphragm castings operate at the extreme frontier of high-temperature aerothermal dynamics. Surviving continuous hot gas streams without trailing-edge cracking, hot corrosion attack, or creep throat distortion demands clean superalloy vacuum metallurgy (FSX-414 / IN-939), intricate ceramic core serpentine cooling, 5-axis CNC airfoil contouring, and zero-defect NDT quality verification.
Partnering with an experienced, integrated precision superalloy casting and machining powerhouse ensures that your gas and steam turbines achieve maximum heat rates, exceptional thermal efficiency, and decades of reliable power generation.
Contact Dandong City Pengxin Machinery Co., Ltd. to submit your turbine guide vane or diaphragm drawings.
Dandong City Pengxin Machinery Co., Ltd. — Heavy Castings and Precision Machining, Since 1958.
Previous: Heavy Mining Electric Rope Shovel & Dragline Castings: High-Strength Steels (ASTM A148 Gr 150-125), Track Shoes, and Boom Point SheavesNext: Casting Simulation: How Digital Technology Optimizes Casting Design Before Metal Is Poured
Products
Hot News
-
Cast Iron Components in Grain Mill Machinery
-
![Your Trusted Partner For Premium Cast Iron Bollards——Pengxin]()
Your Trusted Partner For Premium Cast Iron Bollards——Pengxin
-
![Production and Delivery Delays of Exhaust Manifolds in China]()
Production and Delivery Delays of Exhaust Manifolds in China
-
![Reciprocating & Process Gas Compressor Casing Castings: High-Pressure Hydrogen, Compacted Graphite Iron (CGI / GJV-450), and NACE Compliance]()
Reciprocating & Process Gas Compressor Casing Castings: High-Pressure Hydrogen, Compacted Graphite Iron (CGI / GJV-450), and NACE Compliance


Contact Us
- Phone:+86 15941574876
- Fax:0415-7875330
-
Email:jackma@px-casting.com