Reciprocating & Process Gas Compressor Casing Castings: High-Pressure Hydrogen, Compacted Graphite Iron (CGI / GJV-450), and NACE Compliance
2026-09-13
Reciprocating & Process Gas Compressor Casing Castings: High-Pressure Hydrogen, Compacted Graphite Iron (CGI / GJV-450), and NACE Compliance
Meta Description: A complete technical guide to reciprocating and process gas compressor cylinder and casing castings. Explore Compacted Graphite Iron (CGI / ISO 16112 GJV-450 / GJV-500), high-ductility nodular iron (EN-GJS-400-18-LT), low-temp cast steel (ASTM A352 LCC), hydrogen embrittlement control, NACE MR0175 compliance, and precision CNC crosshead boring.
In petroleum refining, natural gas transmission pipelines, petrochemical synthesis (ammonia, methanol, ethylene), and green hydrogen fueling infrastructure, heavy reciprocating and process gas compressors operate under severe thermodynamic and chemical loads:
- High-Pressure Gas Containment: Multi-stage reciprocating compressor cylinders compress hydrogen (), compressed natural gas (CNG), carbon dioxide (), and sour gas () at dynamic pulsating discharge pressures ranging from ().
- Dynamic Cyclic Inertia & Pressure Pulsations: Operating at 300 to 1,200 RPM, compressor cylinder bodies, cylinder heads, distance pieces, crosshead guides, and crankcases endure continuous multi-axial tensile hoop fatigue (), reciprocating piston reversal shocks, and high thermal compression gradients ().
- Corrosive & Hydrogen Embrittlement Risks: Hydrogen atoms diffusing into high-hardness steel matrices cause rapid Hydrogen-Induced Stress Cracking (HISC), while wet hydrogen sulfide () demands strict compliance with NACE MR0175 / ISO 15156.
Under these hazardous gas conditions, through-wall micro-porosity, cylinder wall weeping, or crosshead guide fatigue cracking presents severe catastrophic explosion and toxicity risks.
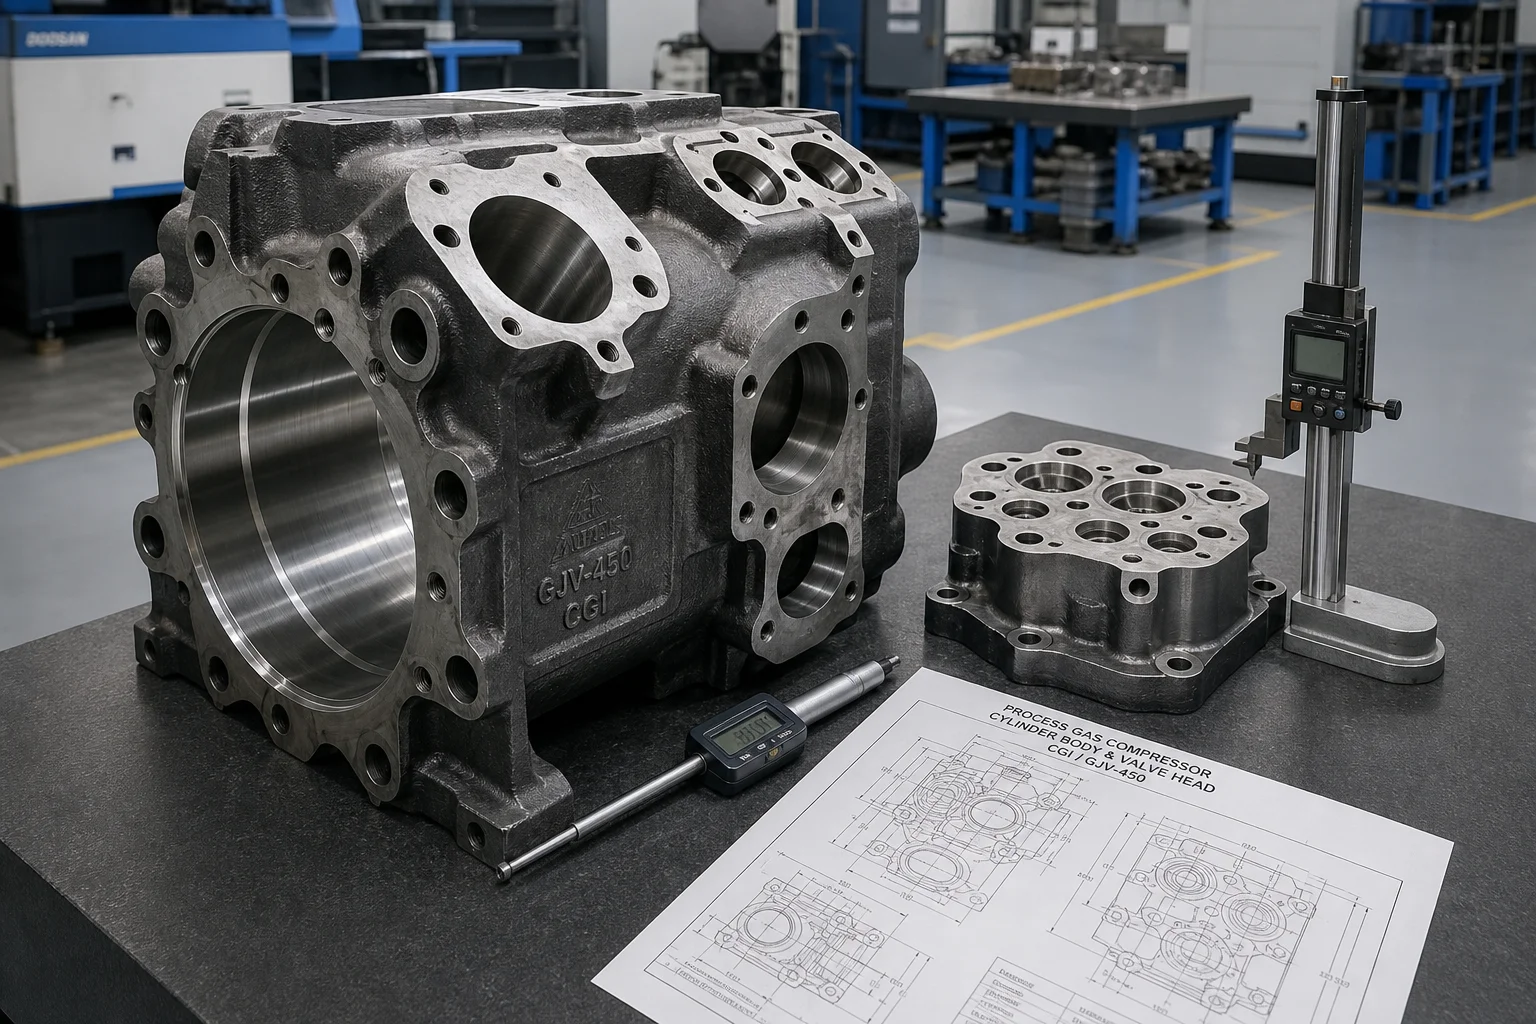
Achieving absolute gas containment requires advanced casting metallurgy: casting Compacted Graphite Iron (CGI / Vermicular Iron / ISO 16112 Grade GJV-450 / GJV-500) to combine the high tensile strength of ductile iron with the superior thermal conductivity and fatigue resistance of gray iron, deploying Low-Temperature Cast Steels (ASTM A352 LCC / ASTM A216 WCC) for hydrogen service, integrating core-supported internal water cooling jackets, and executing precision horizontal CNC boring of cylinder liner cavities, crosshead guides, and valve pockets ().
This comprehensive guide details compressor alloy metallurgy, CGI vermicularity control, internal water jacket casting, CNC multi-axis boring, and gas-tight hydrostatic/helium testing standards.
1. Operating Dynamic Load Fields & Gas Containment Failure Modes
 ┌──────────────────────────────────────────────┐
                     │ High-Pressure Gas Pulsation (150 - 500 bar)  │
                     └──────────────────────┬───────────────────────┘
                                            │
        ┌───────────────────────────────────┼───────────────────────────────────┐
        ▼                                   ▼                                   ▼
┌───────────────────────────────┐ ┌───────────────────────────────┐ ┌───────────────────────────────┐
│ High-Cycle Pressure Fatigue   │ │ Hydrogen Embrittlement (HISC) │ │ Thermal Hot-Spot Distortion   │
│ (Cyclic hoop stress at valve  │ │ (Atomic $H_2$ diffusion into  │ │ (Uneven cylinder gas heating  │
│  pocket transition fillets)   │ │  hardened steel grain bound)  │ │  causing liner out-of-round)  │
└───────────────────────────────┘ └───────────────────────────────┘ └───────────────────────────────┘| Compressor Component | Operating Gas Condition & Pressure | Critical Failure Mode to Prevent | Material Grade Solution |
|---|---|---|---|
| Reciprocating Cylinder Body | High-pressure hydrogen / natural gas () | Cylinder barrel fatigue rupture, valve pocket weeping | Compacted Graphite Iron (CGI GJV-450) / Cast Steel (A352 LCC) |
| High-Pressure Cylinder Head | Peak dynamic compression pressure () | Head flange bending shear, gasket blowout | Quenched & Tempered Cast Alloy Steel (42CrMo4 / A148) |
| Crosshead Guide & Distance Piece | Reciprocating mechanical side-thrust + vapor venting | Crosshead sliding bore galling, structural vibration | High-Dampening Ductile Iron (EN-GJS-500-7 / QT500-7) |
| Compressor Crankcase Frame | High-tonnage crankshaft bearing reaction forces | Bearing saddle fatigue cracking, main frame sag | High-Rigidity Pearlitic Iron (EN-GJL-300 / HT300) |
2. Compressor Metallurgy Hierarchy: CGI vs. Ductile Iron vs. Cast Steel
A. Compacted Graphite Iron (CGI / ISO 16112 Grade GJV-450 / GJV-500)
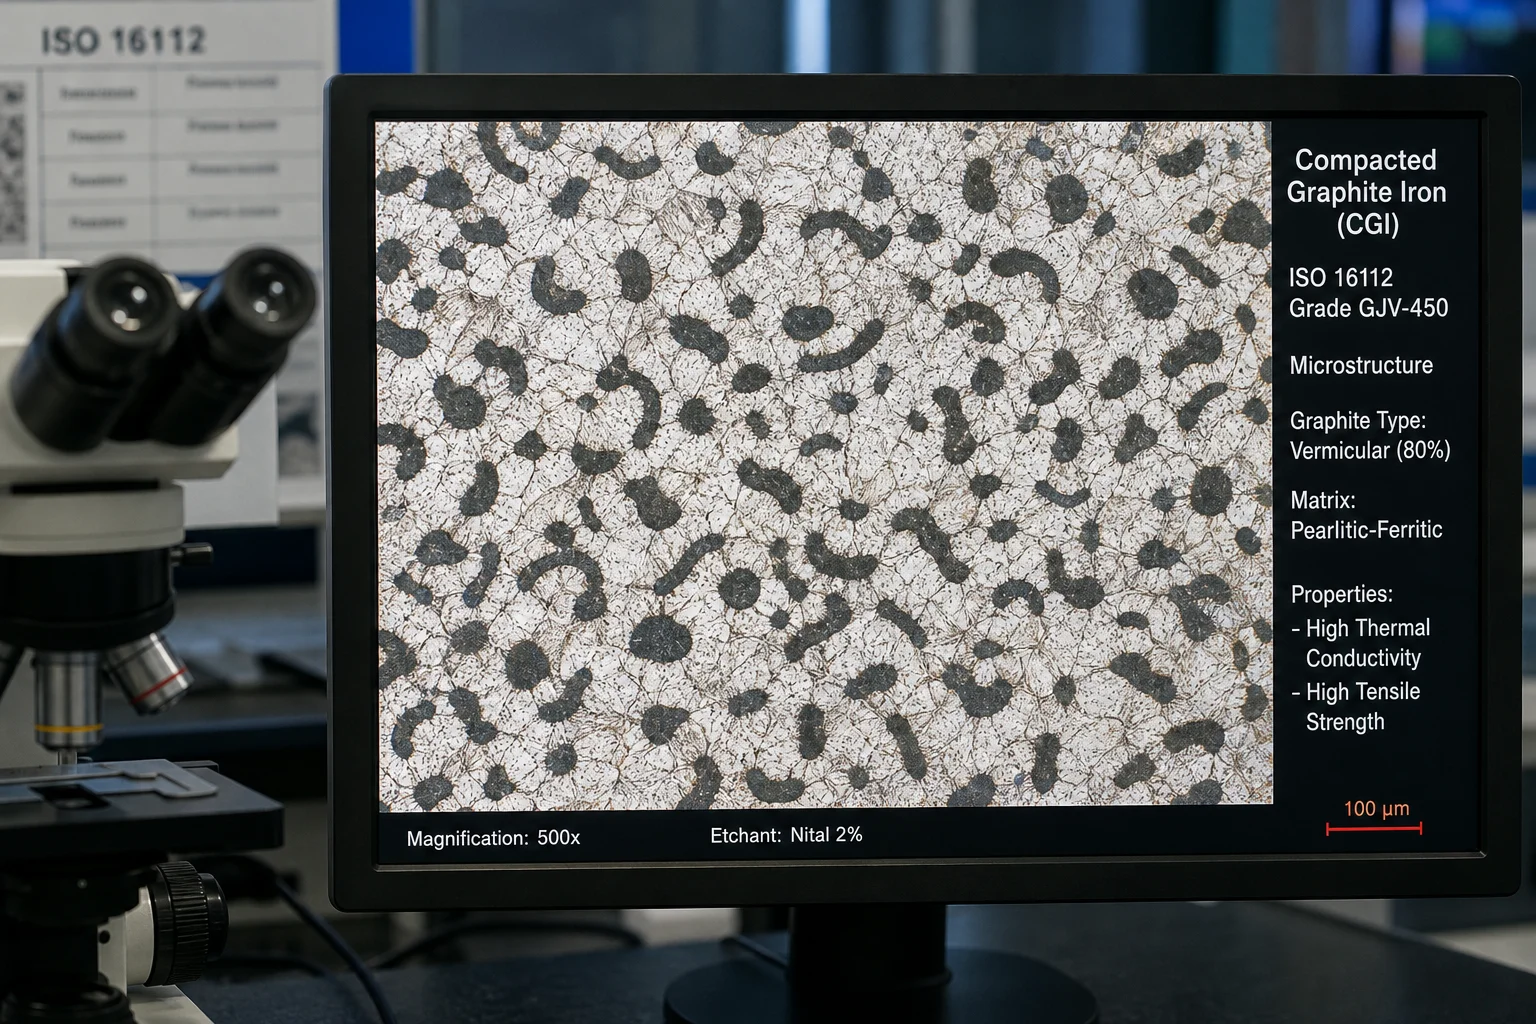
Compacted Graphite Iron (Vermicular Graphite Iron) provides the optimal metallurgical balance for heavy reciprocating compressor cylinders:
- Vermicular Graphite Morphology: Graphite particles exist as short, thick, rounded worm-like clusters with rounded edges ( vermicularity, spheroidal nodules).
- Superior Mechanical Strength: Delivers higher tensile strength () and higher elastic modulus () than standard gray cast iron, resisting high pulsating hoop stresses.
- Superior Thermal Conductivity: Thermal conductivity () is higher than ductile iron, preventing thermal hot spots around discharge valve pockets and eliminating cylinder bore thermal ovalization.
| Property Comparison | Gray Cast Iron (HT300 / GJL-300) | Compacted Graphite Iron (CGI GJV-450) | Ductile Iron (QT500-7 / GJS-500) | Low-Temp Cast Steel (ASTM A352 LCC) |
|---|---|---|---|---|
| Tensile Strength () | ||||
| Yield Strength () | Not Applicable | |||
| Elastic Modulus () | ||||
| Thermal Conductivity () | ||||
| Vibration Damping | High (1.0) | Medium-High (0.6) | Medium (0.3) | Low (0.1) |
| Thermal Fatigue Resistance | Moderate | Superior | Low | Moderate |
B. Low-Temperature Cast Steels for Hydrogen & Sour Gas Service (NACE MR0175)
Where compressor service involves sour gas () or cryogenic gas intake (down to ):
- ASTM A352 Grade LCC: Normalized and tempered carbon-manganese cast steel (, yield ) with verified Charpy impact at .
- NACE Hardness Limitation: To prevent hydrogen-induced stress corrosion cracking (HISCC), maximum hardness is strictly limited to .
3. Directional Solidification & Internal Cooling Jacket Coring
Compressor cylinder castings feature heavy multi-bore box geometries with integrated internal water cooling jackets and suction/discharge gas galleries:
┌─────────────────────────────────────────────────────────────┐
│ 1. 3D Precision Master Tooling & Furan Resin Sand Molding   │
│    • High mold rigidity prevents core shifting or dilation  │
├─────────────────────────────────────────────────────────────┤
│ 2. Phenolic Cold-Box Cores for Water Jackets & Gas Ports    │
│    • Cast-in internal water jackets surrounding the cylinder│
│      bore and suction/discharge valve pockets               │
├─────────────────────────────────────────────────────────────┤
│ 3. Automated Magnesium / Rare-Earth Treatment for CGI Melt  │
│    • Precise thermal analysis (ATAS) controls residual Mg   │
│      within $0.008\% – 0.015\%$ to lock in 75–85% vermicularity│
├─────────────────────────────────────────────────────────────┤
│ 4. Tangential Bottom Ingate System with Ceramic Filters     │
│    • Non-turbulent, clean metal entry; zero slag inclusion  │
└─────────────────────────────────────────────────────────────┘
4. Multi-Axis Horizontal CNC Boring & Valve Pocket Machining
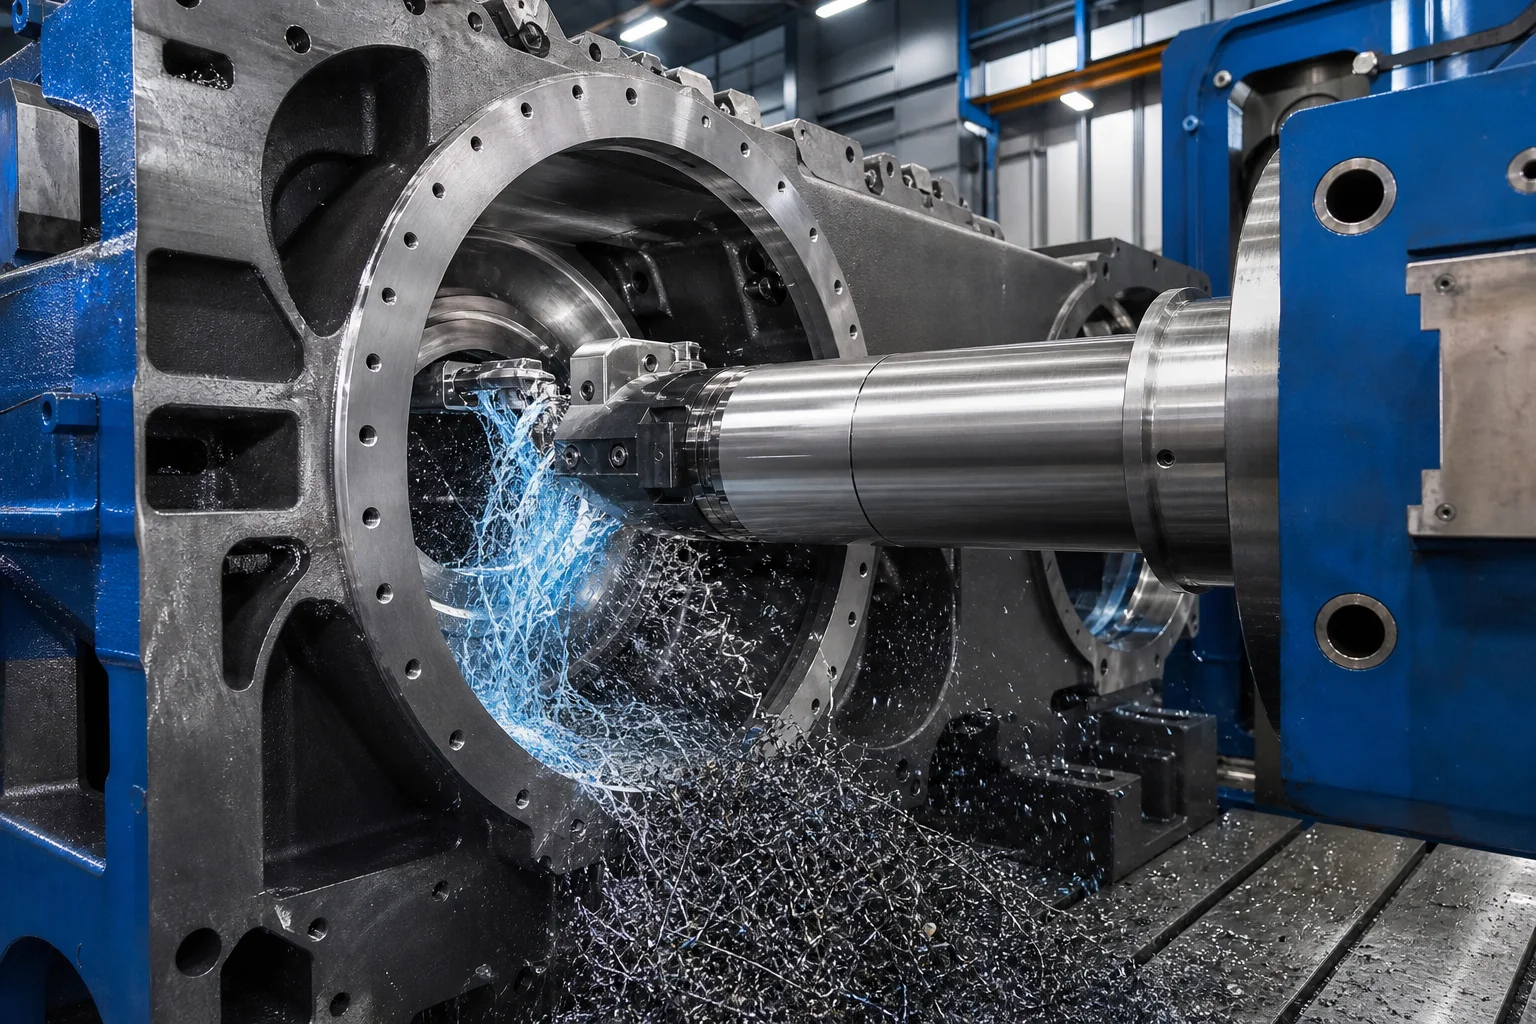
Compressor thermodynamic efficiency and piston ring longevity depend strictly on cylinder bore cylindricity and valve seat concentricity:
 ┌───────────────────────────────────────────────────────┐
        │ 1. Full Stress-Relief Heat Treatment (550 °C – 600 °C)│
        │ • Eliminates casting stresses; guarantees zero drift  │
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 2. Heavy 5-Axis CNC Horizontal Boring Center          │
        │ • Precision boring of cylinder main liner bore        │
        │ • Single-setup boring of crosshead guide cavity       │
        │ • Line-boring coaxiality maintained within $\le 0.025\text{ mm}$│
        └──────────────────────────┬────────────────────────────┘
                                   │
                                   ▼
        ┌───────────────────────────────────────────────────────┐
        │ 3. Suction & Discharge Valve Pocket Precision Machining
        │ • Multi-axis CNC milling of valve sealing counterbores│
        │ • Valve pocket flatness $\le 0.015\text{ mm}$ ($Ra \le 0.4\text{ µm}$)│
        └───────────────────────────────────────────────────────┘
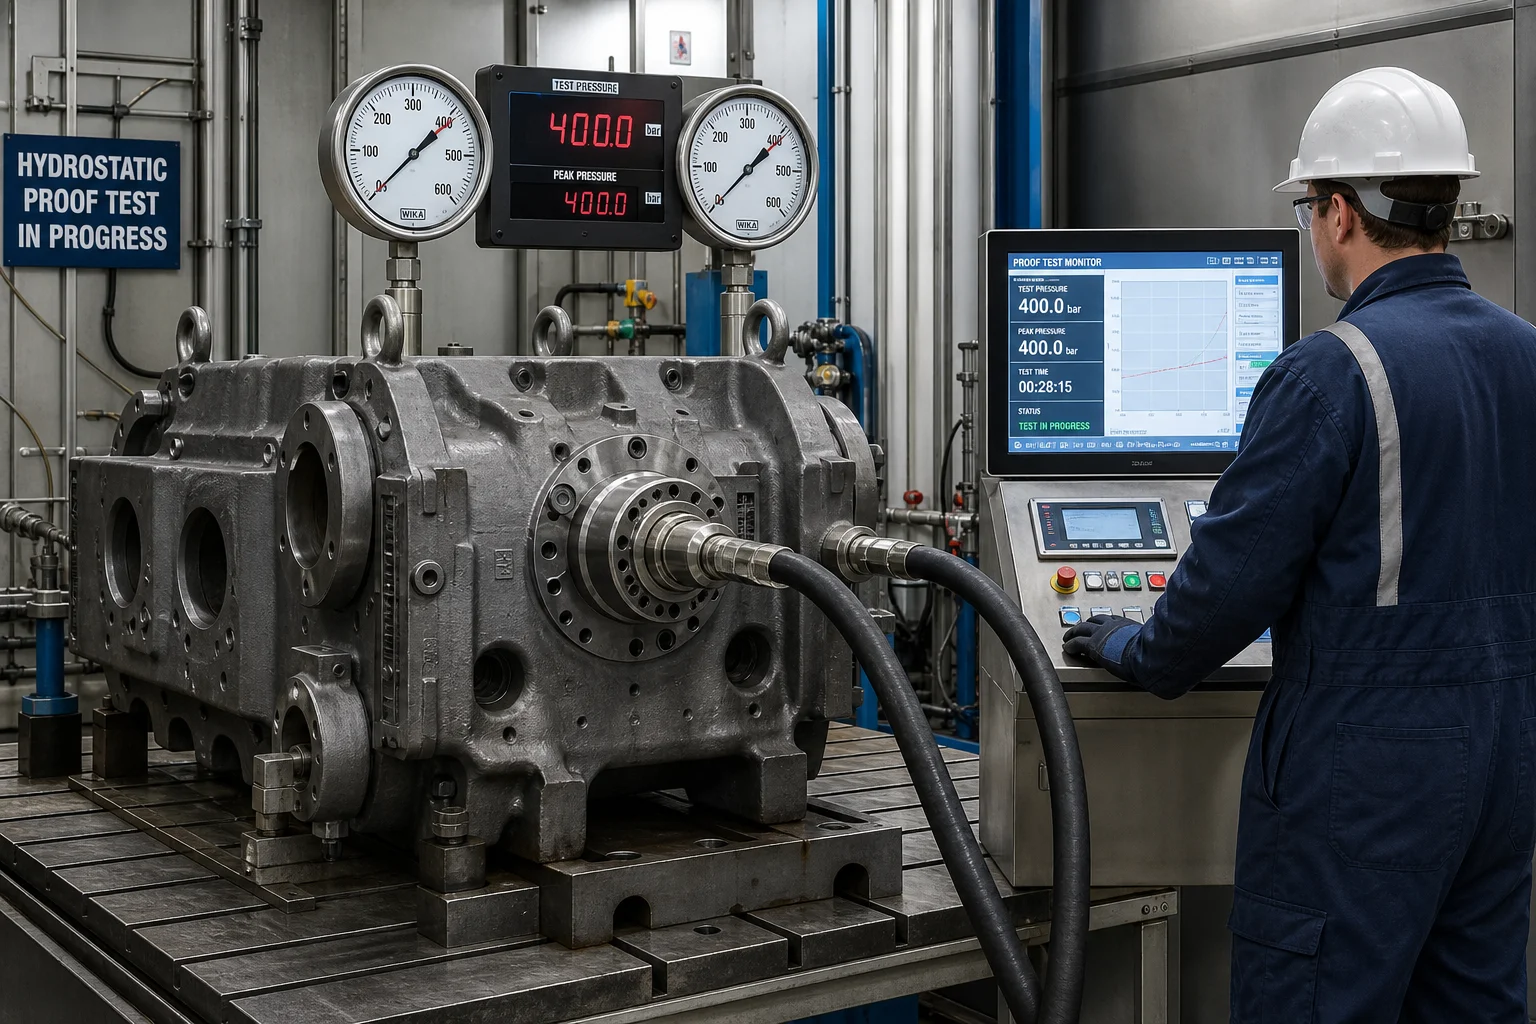
5. Gas-Tight Hydrostatic & Helium Proof Testing Standards
| Quality Inspection Category | Testing Standard | Test Parameter & Acceptance Criteria |
|---|---|---|
| Hydrostatic Cylinder Proof Test | API 618 / ASME Sec VIII Div 1 | maximum allowable working pressure () held for ; zero pressure drop |
| Water Cooling Jacket Hydro Test | API 618 Standard | water pressure held for ; zero seepage into gas chambers |
| Helium Mass Spectrometer Leak Test | ASTM E499 / ASME Sec V Art 10 | High-pressure Helium gas test at rated pressure; leak rate |
| Vermicularity Phase Analysis | ISO 16112 / ASTM A247 | Microstructural verification: vermicular graphite, nodules |
| Ultrasonic Testing (UT) | EN 12680-3 Class 3 / ASTM A609 | 100% volumetric scan on high-pressure cylinder walls and valve bosses; zero shrinkage |
| Magnetic Particle Testing (MT) | EN 10228-1 / ASTM E709 (Fluorescent) | 100% coverage of valve pocket fillets and head flange transitions; zero linear crack indications |
6. Compressor Casting Capabilities at Dandong City Pengxin Machinery Co., Ltd.
Products
Hot News
-
Cast Iron Components in Grain Mill Machinery
-
![Your Trusted Partner For Premium Cast Iron Bollards——Pengxin]()
Your Trusted Partner For Premium Cast Iron Bollards——Pengxin
-
![Production and Delivery Delays of Exhaust Manifolds in China]()
Production and Delivery Delays of Exhaust Manifolds in China
-
![Heavy Mining Electric Rope Shovel & Dragline Castings: High-Strength Steels (ASTM A148 Gr 150-125), Track Shoes, and Boom Point Sheaves]()
Heavy Mining Electric Rope Shovel & Dragline Castings: High-Strength Steels (ASTM A148 Gr 150-125), Track Shoes, and Boom Point Sheaves


Contact Us
- Phone:+86 15941574876
- Fax:0415-7875330
-
Email:jackma@px-casting.com
-
+8615941574876 Scan to chat on WhatsApp
-
 Scan to chat on WeChat
-
Inquiry
-
Back to Top